
Your merchandise should never stop working for your brand, even when the sun goes down. Most custom clothing loses its impact the moment the lights dim, but glow in the dark ink printing turns every t-shirt into a high-impact, light-reactive statement. It is the ultimate way to ensure your fans stand out in a crowded venue, at a late-night festival, or inside a dark club. You want apparel that creates an immediate "wow" factor, but you probably worry that the effect will disappear after a single trip through the washing machine.
We understand the frustration of investing in special effects only to see them fail. You need to know the clear difference between standard neon and true phosphorescent inks, and whether your complex logo is actually suitable for this specialised process. This guide clears up the confusion. We will show you how to achieve professional, long-lasting results that survive the laundry and the mosh pit alike. With over 25 years of industry experience, RAW Merch is here to handle the technical complexity for you. From durability secrets to design tips for 2026, here is everything you need to know about creating high-quality glowing merch right here in the UK.
Key Takeaways
- Master the "Second Design" concept to create merchandise that reveals hidden messages or alternative visuals when the lights go out.
- Learn the technical difference between phosphorescence and fluorescence to ensure your glow in the dark ink printing actually stores light rather than just reacting to UV.
- Prioritise screen printing for bulk orders to achieve the thick ink deposits necessary for the brightest and most durable glow.
- Maximise visual impact by using high-contrast designs on dark base garments like black or navy to make the light-reactive elements pop.
- Work with a UK-based expert to ensure your technical prints meet high wash-fastness standards and arrive in time for your next event or tour.
What is Glow in the Dark Ink Printing? (Definition & Impact)
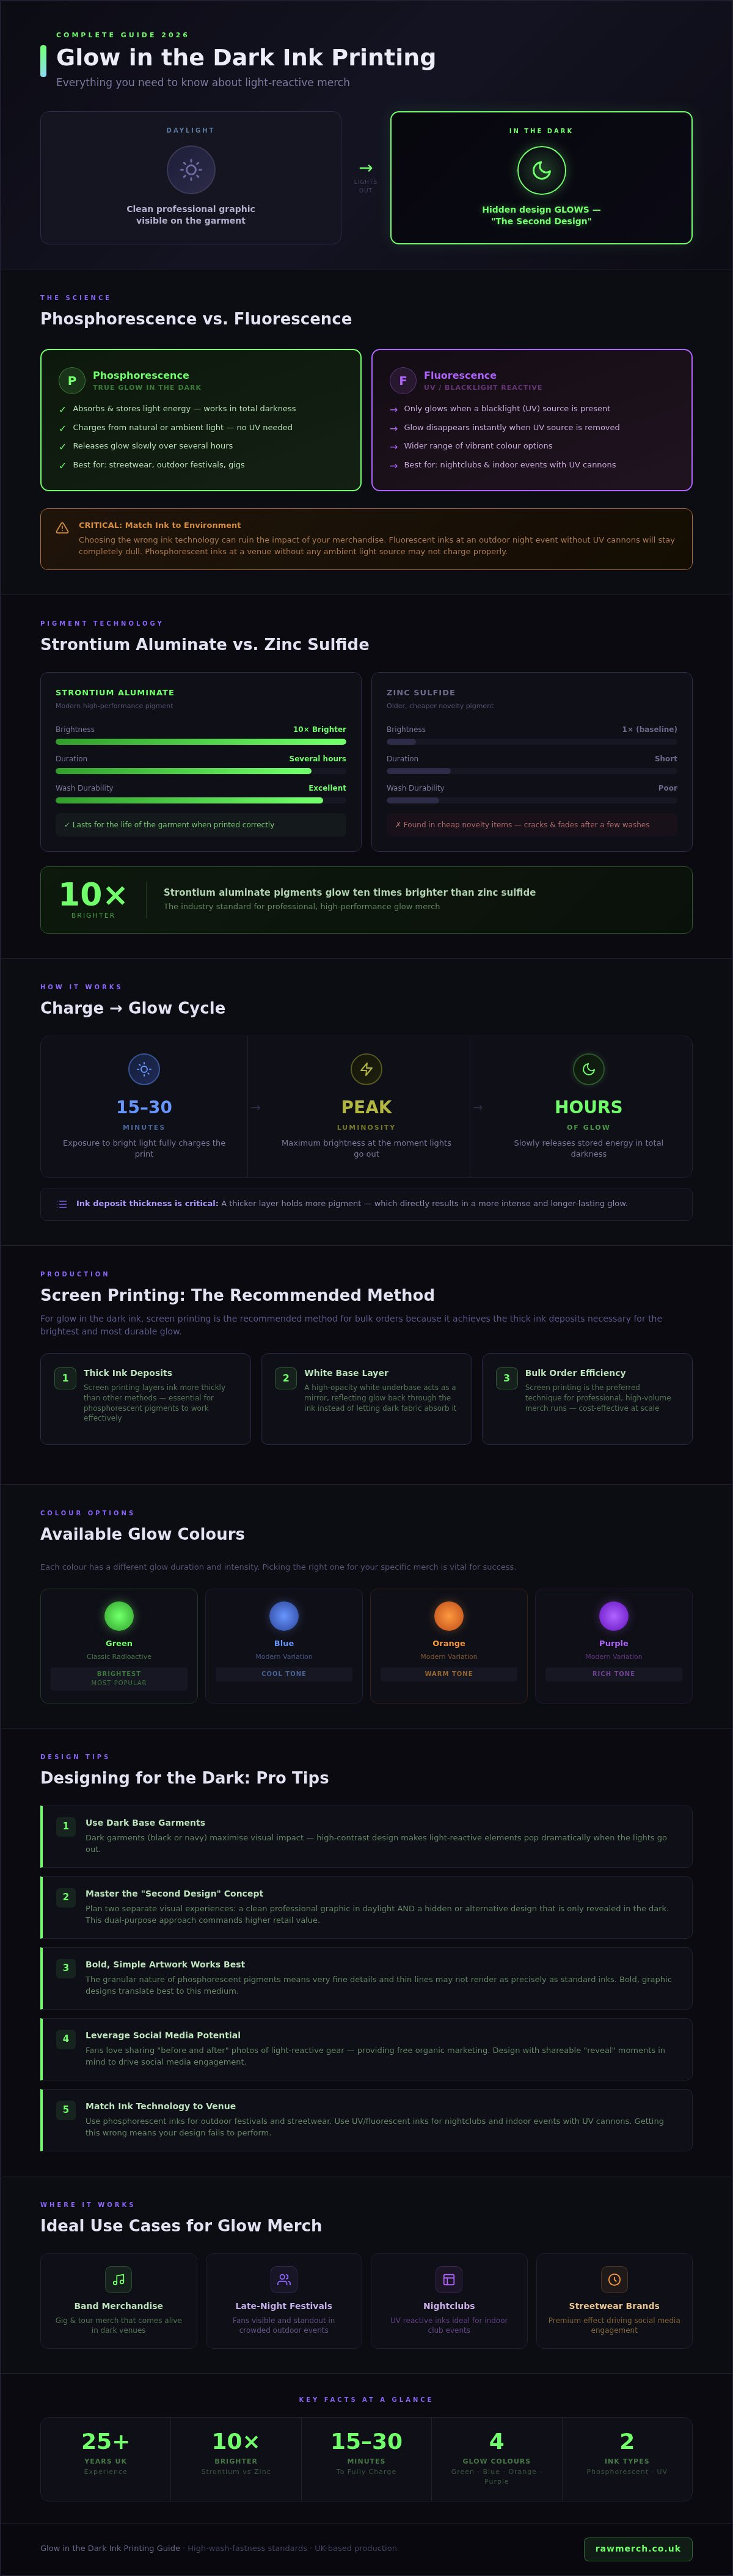
Glow in the dark ink printing is a specialised production technique that uses phosphorescent pigments to create light-reactive apparel. Unlike standard inks that simply sit on the fabric, these inks rely on the science of phosphorescence to absorb ambient light and release it slowly in total darkness. This isn't just about making things "bright". It's about adding a functional, interactive layer to your garments that changes based on the environment. It is a technical process that requires precision, but the results are undeniable.
We call this the 'Second Design' concept. In daylight, your t-shirt or hoodie features a clean, professional graphic. Once the lights go down at a gig or festival, the design transforms into something entirely different. This dual-purpose aesthetic is a massive win for band merchandise and event promoters. It provides fans with a unique experience that standard screen printing cannot match. High-impact visuals like these often command a higher retail value because they offer more than just a logo; they offer a performance. You aren't just selling a shirt; you're selling a "wow factor" that people will pay a premium for.
The Anatomy of a Glow Print
To get the best result, the ink layer must be significantly thicker than a standard plastisol print. These pigments are granular. They need a solid foundation to work effectively. We always recommend a high-opacity white base layer. This acts as a mirror, reflecting the glow back through the ink rather than letting the dark fabric soak it up. While the classic "radioactive green" remains the brightest and most popular option, modern variations now include blues, oranges, and purples. Each colour has a different glow duration and intensity, so picking the right one for your specific merch is vital for success.
Why Brands Choose Glow Ink in 2026
Standing out in 2026 requires more than just a cool graphic. Streetwear brands and festival organisers use glow in the dark ink printing to drive social media engagement. Fans love sharing "before and after" photos of their light-reactive gear, providing you with free organic marketing. Durability has also seen a massive boost. Older versions of these inks used to crack or fade after a few washes, but modern phosphorescent inks are far more resilient. When printed correctly by a seasoned expert, the glow remains vibrant for the life of the garment. It's a reliable, no-nonsense way to add a premium effect without the complexity of electronics.
The Science of Glow: Phosphorescence vs. Fluorescence
Understanding the technical side of glow in the dark ink printing prevents expensive ordering mistakes. Most people use "glow" as a catch-all term, but there is a massive difference between phosphorescence and fluorescence. Phosphorescence is the true "glow in the dark" effect. It absorbs energy from the visible light spectrum and stores it. This energy is then released slowly over time, even in total darkness. Fluorescence, or UV reactive ink, only works when a blacklight is present. If the UV source is removed, the glow disappears instantly.
Choosing the wrong ink technology can ruin the impact of your merchandise. If you sell "glow" shirts for an outdoor night event without UV cannons, fluorescent inks will stay dull. You need to match the ink to the environment where your fans will actually wear the merch. It is about functionality as much as it is about style. Getting this right ensures your fans aren't left in the dark with a design that fails to perform.
How Phosphorescent Inks Work on Fabric
We use strontium aluminate pigments for high-performance merch. These are far superior to the older, weaker zinc sulfide pigments found in cheap novelty items. Strontium aluminate glows ten times brighter and lasts significantly longer. Charge time is the period of light exposure required for the ink to reach its maximum luminosity. Usually, 15 to 30 minutes of bright light is enough to fully power the print for several hours. The thickness of the ink deposit also plays a vital role. A thicker layer of ink holds more pigment, which directly results in a more intense and durable glow.
Choosing Between Glow and UV Reactive
Standard glow is the best choice for streetwear and outdoor festivals. It relies on natural or ambient light to charge up. UV reactive inks are the industry standard for nightclubs and indoor events. They offer a much wider range of vibrant neon colours that "pop" under specialised lighting. You can combine both in a hybrid print for maximum versatility. A hybrid print uses UV ink for daytime vibrancy and phosphorescent ink for a total blackout effect. This adds technical complexity but creates a truly standout piece of merchandise. If you aren't sure which method fits your specific design, consult with our expert team for a technical recommendation.
Printing Methods Compared: Screen Printing vs. Modern Alternatives
Choosing the right production method is critical for the performance of your merchandise. Screen printing remains the industry gold standard for glow in the dark ink printing. It offers the thickest ink deposit, which is essential for a powerful, long-lasting glow. Modern alternatives like DTF (Direct to Film) are gaining ground for smaller, detailed runs, while vinyl heat transfer remains a fallback for ultra-simple, one-off designs. Each method has a different impact on the feel, durability, and cost-effectiveness of your apparel.
You need to balance the complexity of your artwork against the desired brightness of the glow. While digital methods offer more flexibility for intricate colours, they rarely match the sheer luminosity of traditional ink. We prioritise methods that ensure your fans get a product that works as advertised. It is about choosing the right tool for the specific job, whether that is a 500-piece tour run or a limited-edition streetwear drop.
Why Screen Printing Wins for Bulk Orders
Screen printing is the most reliable way to lay down a thick, consistent ink deposit. Because phosphorescent pigments are heavy, they need a robust application to reach maximum luminosity. It is the most cost-efficient method when you are printing 50 or more units for tours, retail, or promotional events. Longevity is another massive advantage. A professionally screen-printed glow design can survive 50 or more washes without losing its reactive properties. This makes it the go-to choice for high-quality band merch that needs to survive life on the road and frequent cleaning.
DTF and Special Effects: The New Frontier
DTF technology allows us to apply glow effects to complex, multi-colour designs that were previously impossible with traditional methods. Understanding what is a vector based image is crucial here, as these files allow for precise glow borders around intricate graphics. You should choose DTF when you need detailed accents rather than a solid block of glow. However, digital glow has limitations. The ink layer is thinner than screen printing, which means the glow duration is usually shorter. It is a trade-off between design complexity and total light output.
Quick Comparison of Methods:
- Screen Printing: Heavy ink deposit, maximum durability, best for bulk orders.
- DTF: Softer hand feel, great for detail, ideal for small to medium runs.
- Vinyl: Rubbery feel, limited to simple shapes, best for one-offs or samples.
Designing for the Dark: Pro Tips for High-Impact Merch
Designing for glow in the dark ink printing requires a different mindset than standard merch. Contrast is your most powerful tool. For the glow to pop, you need a dark background. Black, navy, and charcoal fabrics provide the necessary negative space to make the phosphorescent ink stand out. If you print on a white shirt, the glow will be almost invisible because the fabric itself reflects too much ambient light. You should also consider placement. Areas like the chest and back catch more overhead light during the day, ensuring the ink is fully charged for the night.
Use the 'Hidden Message' technique to create interactive merch that surprises your fans. You can print a standard design in one colour and then use glow ink for a specific word or graphic that only appears in the dark. This turns a simple garment into a conversation piece. Avoid fine lines in these glow-enabled areas. Tiny details often fail to glow effectively because they cannot hold enough pigment. Keep your glow elements bold and chunky to ensure your glow in the dark ink printing achieves maximum light emission.
Selecting the Right Garment
Heavyweight cotton is the gold standard for special effect inks. It provides a stable, flat surface that handles the thick ink deposits required for a professional finish. While you can use blends, 100% cotton usually offers better ink adhesion and long-term durability. You aren't limited to t-shirts either. We see incredible results on accessories like custom bobble hats where a glowing logo adds a premium feel. Remember that glow ink has a natural off-white or pale lime colour in daylight. Ensure this fits your brand's colour palette before committing to a full production run.
Preparing Your Artwork Files
High-quality production starts with the right files. Vector files are non-negotiable for screen printing because they allow us to create the sharp, clean screens needed for heavy ink. You must separate your 'glow layer' from the standard colours in your design software. This allows us to treat it as a separate pass on the press. Overprinting is the process of layering glow ink on top of standard colours. This technique can add depth but requires expert execution to avoid muddy results. Our team can help you refine these technical details to ensure the final product looks exactly like your vision.
Ready to see your designs light up the night? Get a professional quote for your custom glow merch today.
Custom Glow Merch with RAW Merch: UK Expertise You Can Trust
You need a partner who understands the technical nuances of glow in the dark ink printing. We bring over 25 years of industry experience to every project we handle. We know exactly how these specialised inks behave on every fabric type, from heavyweight cotton to technical blends. RAW Merch isn't just a supplier; we are your production department. We handle the technical "fiddly" bits that cause other printers to struggle. This ensures your merch is tour-ready and high-impact the moment it arrives.
Choosing a UK-based partner is about more than just geography. It is about reliability and speed. You won't face the "China-shipping" delays or customs headaches that frequently ruin launch schedules. Our production and distribution happen right here in the UK. This allows us to meet tight deadlines for tours, festivals, and product launches with absolute confidence. We provide an end-to-end service that covers everything from initial design consultation to final fulfillment and distribution.
Our No-Nonsense Process
We don't leave anything to chance. It starts with a design consultation where we check your artwork to ensure the glow will actually work as intended. If a detail is too fine or a placement is ineffective, we will tell you. We then move to sampling and quality control. This stage ensures the "charge" time and "glow" intensity meet our strict standards before the full run begins. Finally, our bulk production team follows a reliable schedule to hit your event or launch date every single time.
Ready to Light Up Your Brand?
Waiting for cheaper overseas shipping can destroy a marketing campaign. A three-week delay might mean missing your biggest tour date or the most important event of the year. We eliminate that risk by keeping everything local and efficient. Whether you need a limited run of streetwear hoodies or thousands of promotional items, we provide a tailored service that prioritises execution. You get high-quality merch that your fans will love, delivered exactly when you need it. Don't settle for "maybe" when it comes to your brand's reputation.
GET A QUOTE FOR YOUR GLOW MERCH
DOMINATE THE DARKNESS WITH PROFESSIONAL GLOW MERCH
Your brand deserves more than a standard t-shirt. By mastering the technical side of glow in the dark ink printing, you create an interactive experience that fans will talk about long after the lights come up. You now know that true phosphorescent ink offers the best results for outdoor events, while high-contrast designs on heavyweight cotton ensure your message stays visible. Don't let technical confusion or shipping delays from overseas hold back your next launch.
At RAW Merch, we bring over 25 years of UK-based industry experience to your project. We are specialists in high-durability screen printing and fulfillment for touring bands; we ensure your gear survives every wash and every venue. We handle the technical complexity so you can focus on your creative vision. It's time to turn your concepts into high-impact, light-reactive merchandise that truly stands out in a crowded market. Take the next step and secure your production slot with a partner you can trust.
GET YOUR CUSTOM GLOW MERCH QUOTE
GLOW IN THE DARK INK PRINTING: FREQUENTLY ASKED QUESTIONS
Does glow in the dark ink eventually stop working?
High-quality phosphorescent ink will continue to recharge and glow for years. It doesn't have a battery life that eventually runs out. The effect relies on a physical reaction within the pigment itself. While the glow remains functional, the print may show signs of wear after many years of heavy use. We use industrial-grade binders to ensure the ink stays bonded to the fabric for the long term. This provides a durable result for any brand.
Can you print glow in the dark ink on white t-shirts?
You can print on white garments, but we don't recommend it for maximum impact. Glow in the dark ink printing requires a dark background to create the necessary contrast. On a white t-shirt, the fabric reflects too much ambient light, which washes out the glowing effect. For the best results, stick to black, navy, or charcoal. This ensures your design is actually visible when the lights go down and the crowd arrives.
Is glow in the dark ink safe for skin and children's clothing?
Yes, modern phosphorescent inks are non-toxic and safe for all ages. We use specialised pigments that meet strict UK safety standards for apparel. These inks don't contain radioactive materials or harmful chemicals that irritate the skin. You can confidently use this effect for children's merchandise, school leavers' hoodies, or retail fashion lines. It's a safe, reliable way to add a unique feature to any custom clothing project without compromising on health or safety.
How do I wash a t-shirt with glow in the dark printing?
Treat your glow merch like any high-end screen-printed garment. Turn the t-shirt inside out before washing to protect the ink surface from abrasion. Use a cool wash cycle at 30 degrees and avoid harsh detergents or bleach. Never iron directly onto the print, as high heat can damage the specialised pigments. Air drying is always better than tumble drying to maintain the luminosity and prevent the print from cracking over time. Follow these steps for longevity.
What colour does glow in the dark ink look like in the daylight?
Most glow inks have a pale, off-white or light lime-green appearance in normal daylight. They are translucent, which means they can slightly take on the colour of the ink or fabric underneath. If you want a specific look during the day, we can overprint the glow ink onto a standard colour. This allows your design to look professional in the sun while transforming into a vibrant green or blue in the darkness. It's a versatile choice.
Is there a minimum order quantity for glow in the dark printing?
Minimum order quantities for glow in the dark ink printing depend on the chosen production method. For traditional screen-printed glow ink, we typically start at 25 or 50 units to keep the setup costs efficient for you. This is the best route for bulk band merch or promotional runs. If you need a smaller batch, we can discuss modern digital alternatives like DTF. We always aim to find a solution that fits your specific project and budget.
Can I use glow ink with complex, multi-coloured logos?
You can definitely integrate glow effects into complex, multi-coloured logos. We often treat the glow as a separate spot colour layer in the design file. This allows us to highlight specific parts of your logo while keeping the rest of the graphic standard. It works exceptionally well for adding outlines, hidden text, or glowing eyes to intricate artwork. Our team checks every design to ensure the glow elements don't get lost in the detail. We prioritise clarity.
How long does the glow effect typically last after a full charge?
A high-quality print will typically glow for 30 minutes to several hours after a full charge. The duration depends heavily on the thickness of the ink deposit and the intensity of the light source used to charge it. Direct sunlight or bright LED lights provide the fastest, strongest charge. We use premium strontium aluminate pigments to ensure your merchandise stays visible for as long as possible during a gig or event. It's built to last the night.